Delivering end-to-end medical supply chain integration under strict ISO 13485 and WHO regulatory compliance.
We specialize in the manufacturing and global distribution of a wide range of medical products, including hospital equipment, medical disposables, surgical dressings, laboratory products, and home healthcare solutions. With a strong commitment to the principle of "quality first, customer foremost," we have earned the trust and recognition of clients across international medical markets.
Our product portfolio is designed to meet the diverse needs of hospitals, clinics, laboratories, and distributors, ensuring reliable performance, safety, and compliance with international standards. From essential medical consumables to advanced diagnostic and laboratory support products, we strive to deliver consistent quality and value.
Our experienced foreign trade team possesses in-depth knowledge of international trade procedures, regional medical regulations, and cross-cultural communication. This enables us to provide efficient and professional support throughout every stage of cooperation. We aim to be a true one-stop supplier, offering integrated services including consultation, sourcing, order tracking, and after-sales support.
Explore our certified bio-processing, cold storage, and diagnostic systems.
Analyzing the interplay between advanced bio-pharmaceutical manufacturing, cold-chain logistics, and point-of-care delivery systems.
The global market for vaccination supplies has evolved from basic mass-production of standard injection devices to a highly specialized, technology-driven ecosystem. Modern immunization programs demand absolute integrity at every stage of the supply chain—from high-purity upstream filtration systems used in antigen manufacturing to ultra-low temperature cold storage units and sterile, precise delivery devices.
As a leading China-based custom OEM vaccination supplies factory and exporter, our operations bridge the gap between rigorous scientific engineering and large-scale manufacturing efficiency. We provide contract procurement partners, government health ministries, and multinational pharmaceutical enterprises with scalable, customized hardware solutions built to exceed WHO PQS (Performance, Quality, and Safety) benchmarks.
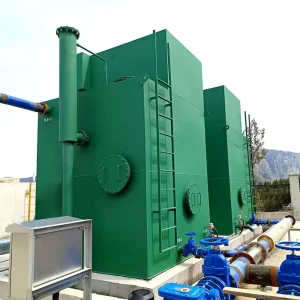
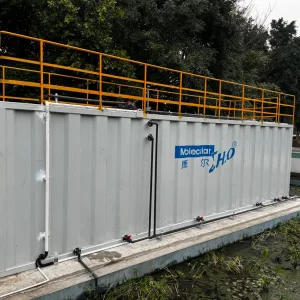
High-yield bio-processing relies on advanced separation technologies. Our crossflow filtration membrane systems and industrial water clarification modules guarantee that base media and active biopharmaceutical components maintain ultra-high purity levels prior to formulation.
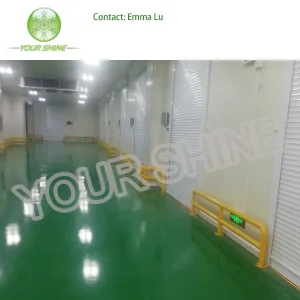
Biological stabilization requires precise temperature controls. Our range of low-temperature water-cooled condensing units and custom refrigeration chillers ensure strict +2°C to +8°C or ultra-low -80°C thermal retention throughout storage and transport transit.
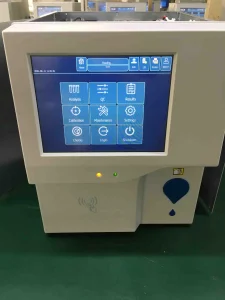
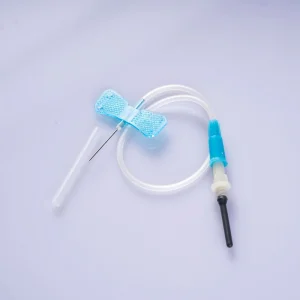
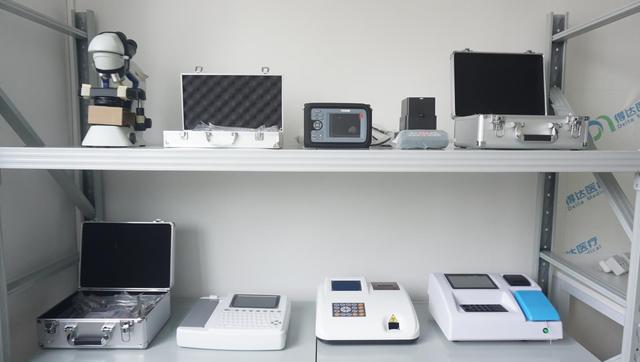
Accurate epidemiology hinges on secure sampling. We deliver high-grade viral transport medium (VTM) kits, precision blood collection butterfly needles, and automated hematology analyzers for real-time post-vaccination monitoring.
Key technological vectors driving efficiency, sustainability, and compliance in global medical exporting.
The rapid rise of mRNA platform vaccines demands specialized sub-zero and ultra-low cold storage solutions. Modular refrigeration units featuring redundant condensing technology are replacing legacy cooling systems.
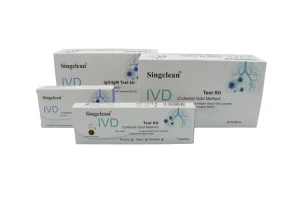
Point-of-care antigen and antibody testing kits are now bundled alongside vaccination drives to assess community baseline immunity and track seroprevalence in real time.
Health authorities are prioritizing contract OEM partners capable of rapidly customizing product packaging, labeling, and specialized consumable sizes to fit localized regional distribution hubs.
Regulatory bodies are enforcing stricter environmental disposal requirements. OEM suppliers are transitioning to recyclable polymers and energy-efficient water treatment processes in medical device assembly.
How our engineered medical systems operate across real-world medical infrastructure environments.
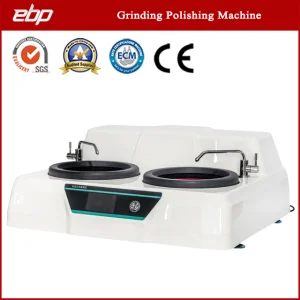
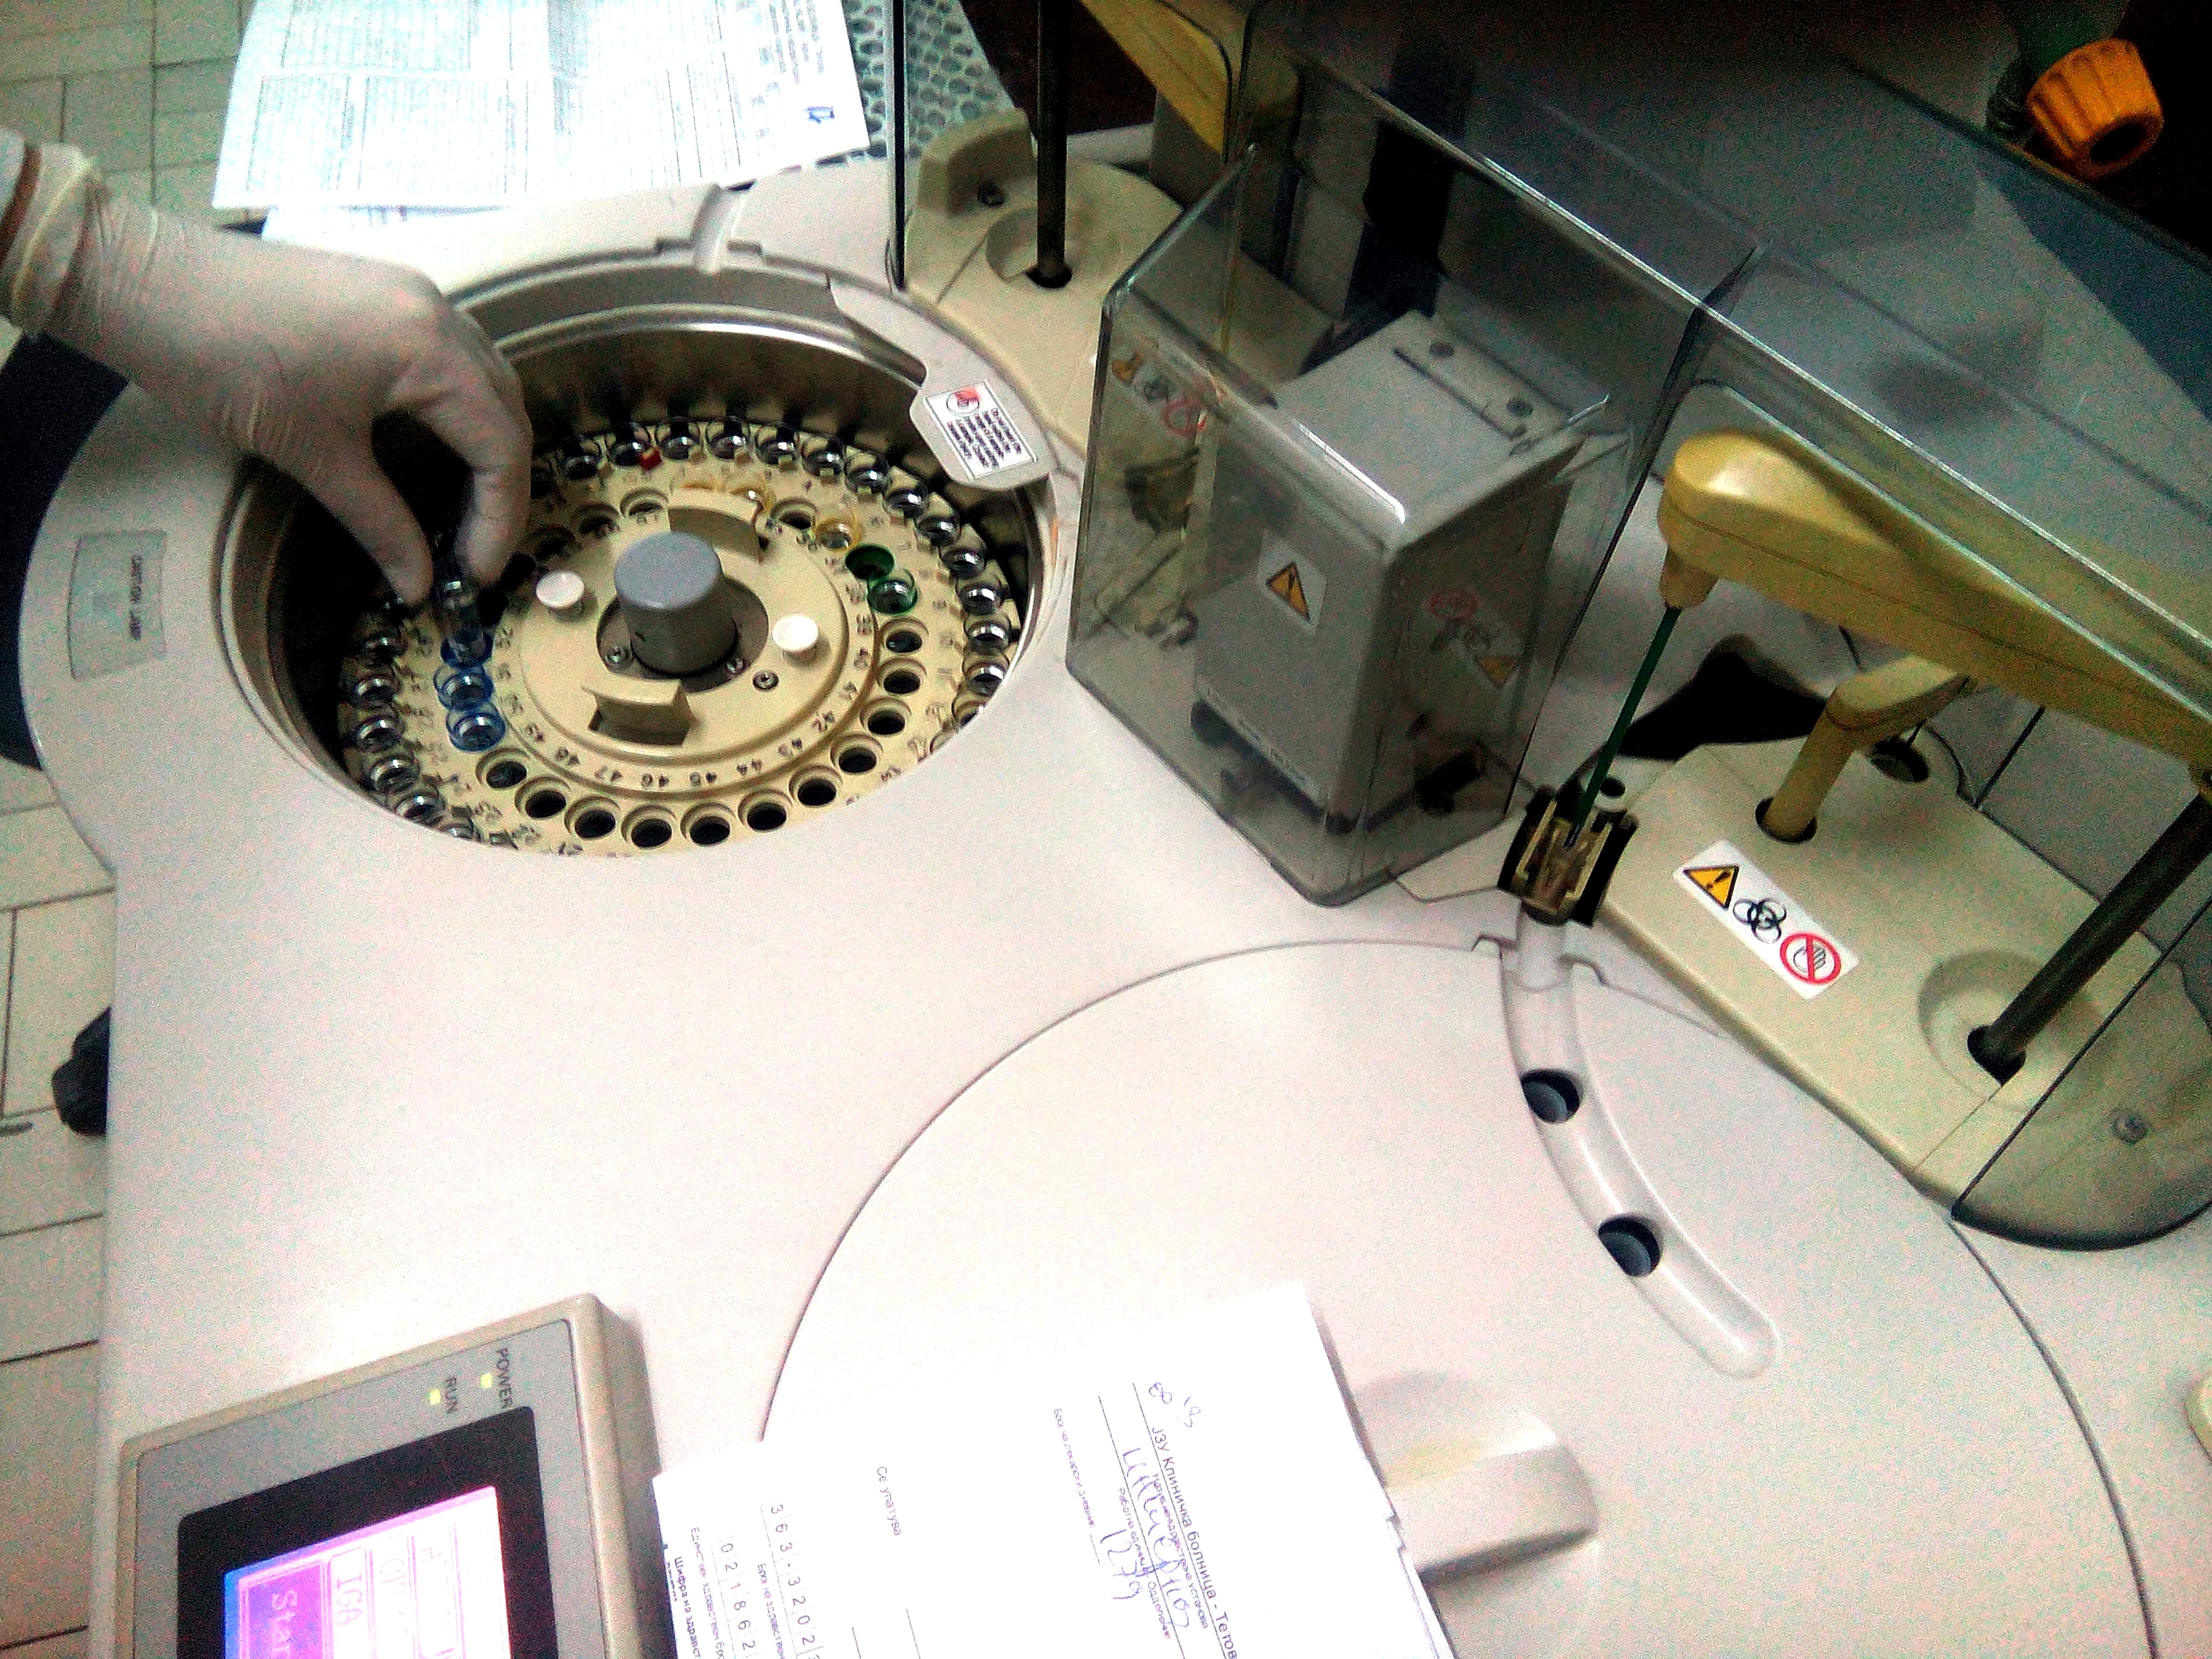
In urban hospital centers and diagnostic laboratories, automated workflow is paramount. Our 3-part hematology analyzer and blood gas analyzers deliver fast, precise blood panel profiling, allowing clinicians to screen patient eligibility prior to administering complex biological therapeutics.
Deploying vaccines in hard-to-reach geographical regions requires lightweight, unbreakable equipment. Our viral sampling swabs paired with 3ml VTM tubes ensure biological sample integrity during transport back to central analytical labs under variable field conditions.
Vaccine production plants generate specific bio-wastewater streams. Our integrated water clarification, membrane crossflow filtration, and textile/chemical wastewater treatment setups enable zero-liquid-discharge (ZLD) strategies and 95% water reuse for bio-pharmaceutical manufacturing plants.
Pioneering intelligent manufacturing, IoT cold chains, and next-generation bio-assay platforms.
Integration of micro-sensor arrays directly into low-temperature water-cooled condensing units and mobile transport boxes. Real-time cellular IoT telemetry monitors internal temperature fluctuations, humidity, and location tracking down to individual batch lots.
Expanding cleanroom Class 100,000 automated injection molding for viral swabs, butterfly needles, and micro-reaction cuvettes. Laser inspection vision systems guarantee 100% dimensional accuracy and eliminate particulate contamination risks.
Incorporating neural network optical engines into benchtop hematology and blood gas analyzers. Rapid recognition of blood cell morphological anomalies reduces diagnostic turnaround time from hours to seconds.
Commercializing fully biodegradable synthetic drapes, eco-conscious sample tubes, and high-flux low-energy crossflow filtration membranes designed to minimize the carbon footprint of global immunization operations.
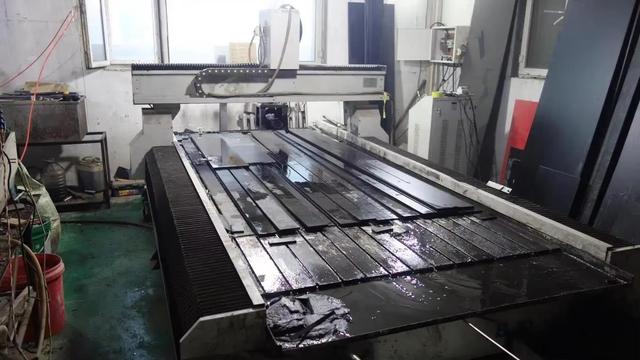
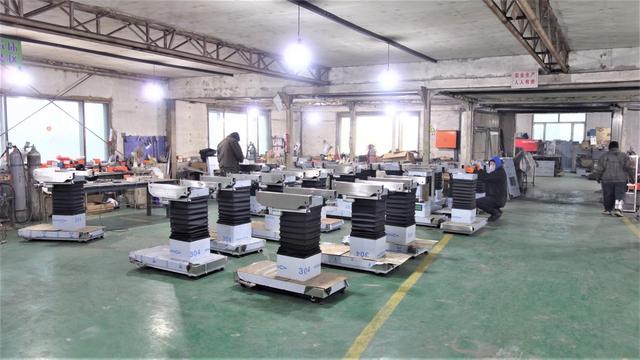
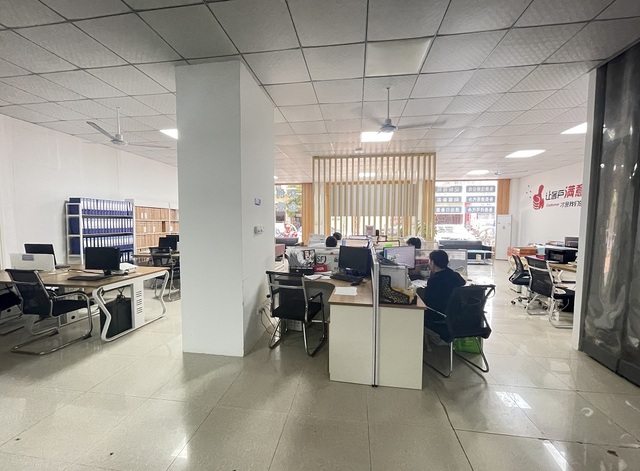
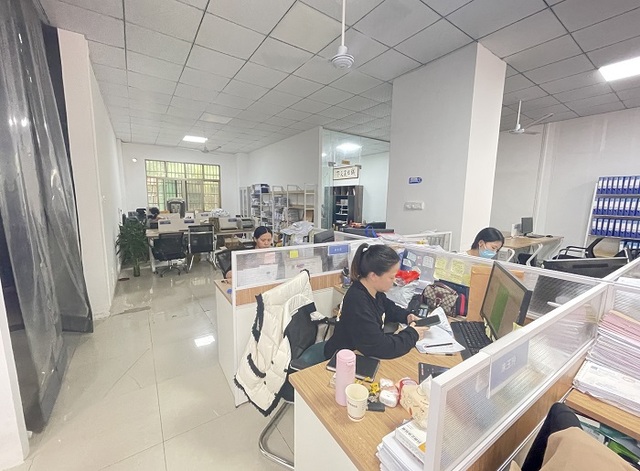
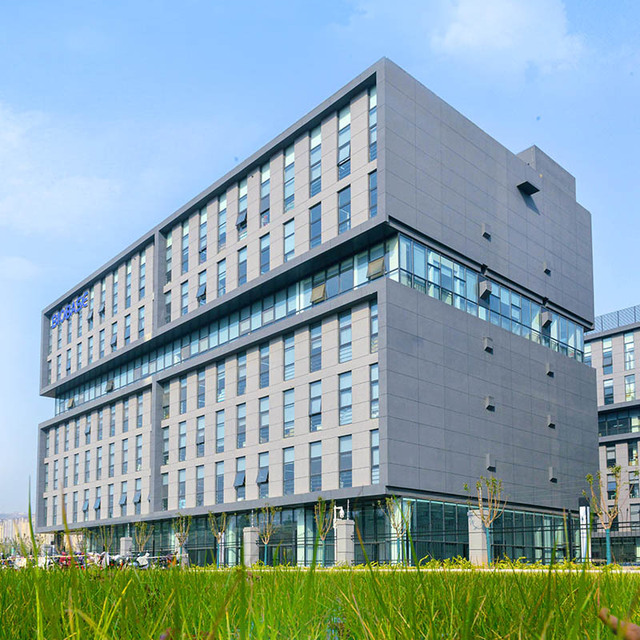
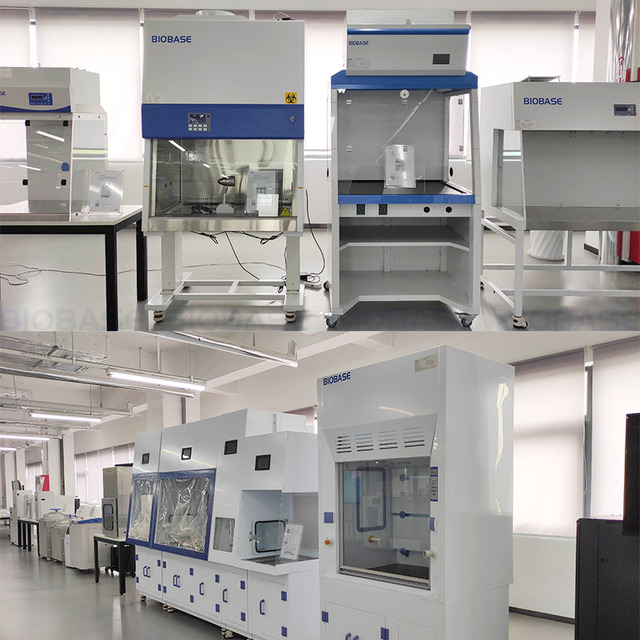
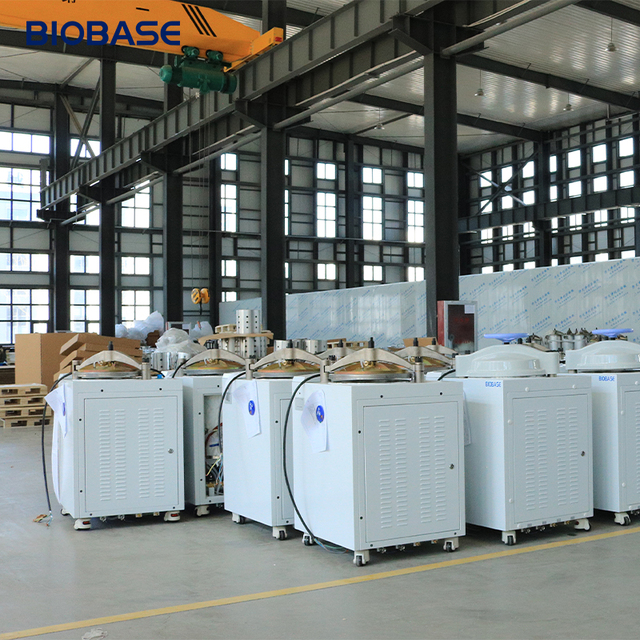
Inside our China-based manufacturing hubs engineered for high-capacity OEM delivery.
As a professional medical device supplier based in China, we adhere to the philosophy of “Quality First, Customer Supreme.” Backed by lean manufacturing capabilities and strict quality control systems, we are dedicated to building long-term partnerships and delivering dependable healthcare solutions to customers worldwide.
Expert insights into custom contract manufacturing, quality certifications, and global export logistics.
We provide comprehensive OEM/ODM customization including custom branding, volumetric tube dimensions, custom viral transport medium (VTM) formulation, needle gauge/tubing lengths for butterfly sets, localized packaging (blister packs, multi-language artwork), and specialized cleanroom kit bundling.
Our manufacturing infrastructure operates under strict ISO 13485 quality management systems. Disposables undergo validated Ethylene Oxide (ETO) or Gamma Irradiation sterilization processes, accompanied by batch-specific Certificates of Analysis (CoA) and Sterility Assurance Certificates.
Standard lead times range from 15 to 30 days depending on customization complexity and volume. Our dedicated foreign trade team handles end-to-end export documentation, sea/air freight booking, and customs clearance support to ensure uninterrupted delivery schedules.
Yes. Our low-temperature water-cooled condensing units and cold storage chillers feature precision digital microprocessor controls, automated defrost cycles, and dual-compressor redundancy designed to maintain strict temperature bands (+2°C to +8°C / -20°C to -80°C) even under high ambient tropical climates.
Explore our sterile disposables, assay kits, and specialized laboratory equipment.

 Mosholu Medical