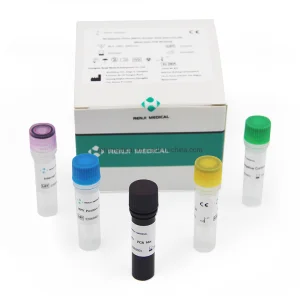
High-precision real-time nucleic acid testing instruments and automated microfluidic workflows engineered for clinical reliability and regional disease surveillance.
Strategic Insights for Healthcare Procurement Directors, Reference Laboratories, and Regional Infectious Disease Monitoring Hubs.
As Grenville continues to elevate its healthcare capabilities, the demand for precise, automated, and rapid molecular diagnostic equipment has escalated. Operating within maritime island climates presents unique operational challenges, including high relative humidity, fluctuating supply chain cycles, and the urgent necessity for decentralized testing. Molecular diagnostic instruments deployed in Grenville require robust thermal stability, zero-cross-contamination architecture, and direct compliance with international IVD directives to handle endemic arboviruses (such as Dengue and Zika), respiratory pathogens, and cervical screening initiatives effectively.
Modern diagnostic procurement networks servicing Grenville require end-to-end reliability. Global healthcare buyers prioritize equipment manufacturers capable of delivering ready-to-deploy hardware, standardized consumable cartridges, and automated reagent preparation units. By integrating automated microfluidic micro-chips and high-throughput extraction workflows, laboratory centers in Grenville reduce hands-on technician time by over 70%, ensuring repeatable diagnostic metrics and minimal error rates in critical clinical evaluations.
Engineered to meet international clinical diagnostic thresholds and environmental adaptability requirements for Grenville facilities.
| System Category | Technical Feature / Parameter | Operational Value for Grenville Labs | Clinical & Regulatory Standard |
|---|---|---|---|
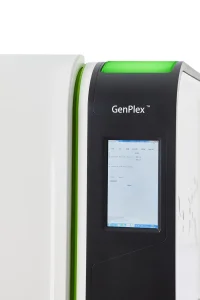
| Real-Time qPCR Platforms | Multi-channel fluorescence (FAM, HEX, ROX, CY5), Solid-state Peltier control | Ensures high-throughput multiplex pathogen screening with ±0.1°C uniformity. | CE-IVD, ISO 13485 Compliance |
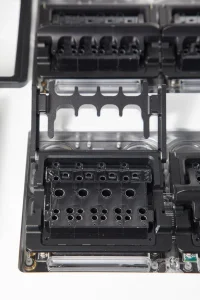
| Microfluidic Chip Systems | Lab-on-a-chip closed liquid path, sub-microliter reagent consumption | Eliminates environmental contamination; drastically reduces expensive reagent shipping mass. | GMP Class 10,000 Production |
| Automated Liquid Filling & Packing | Vision-guided precision capping, automated peristaltic fill modules | Scales local kit production for diagnostic exporters and regional supply centers. | Industrial Automation ISO 9001 |
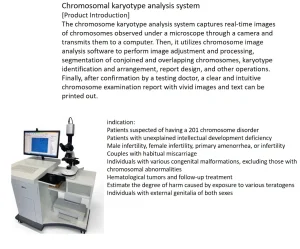
| Karyotype & Cytogenetic Analyzers | High-resolution digital imaging, automated slide scanning, FISH/CGH software | Streamlines oncology and genetic aberration research with AI-driven detection support. | Clinical Genetic Diagnostic Grade |
We specialize in the manufacturing and global distribution of a wide range of medical products, including hospital equipment, medical disposables, surgical dressings, laboratory products, and home healthcare solutions. With a strong commitment to the principle of “quality first, customer foremost,” we have earned the trust and recognition of clients across international medical markets.
Our product portfolio is designed to meet the diverse needs of hospitals, clinics, laboratories, and distributors, ensuring reliable performance, safety, and compliance with international standards. From essential medical consumables to advanced diagnostic and laboratory support products, we strive to deliver consistent quality and value.
Our experienced foreign trade team possesses in-depth knowledge of international trade procedures, regional medical regulations, and cross-cultural communication. This enables us to provide efficient and professional support throughout every stage of cooperation. We aim to be a true one-stop supplier, offering not only a comprehensive range of medical products but also integrated services including consultation, sourcing, order tracking, and after-sales support.
As a professional medical device supplier based in China, we adhere to the philosophy of “Quality First, Customer Supreme.” Backed by lean manufacturing capabilities and strict quality control systems, we are dedicated to building long-term partnerships and delivering dependable healthcare solutions to customers worldwide.
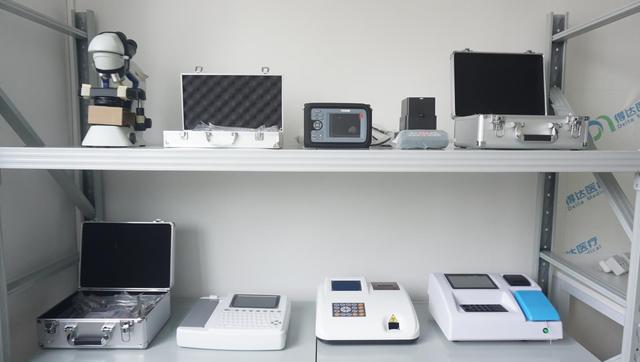
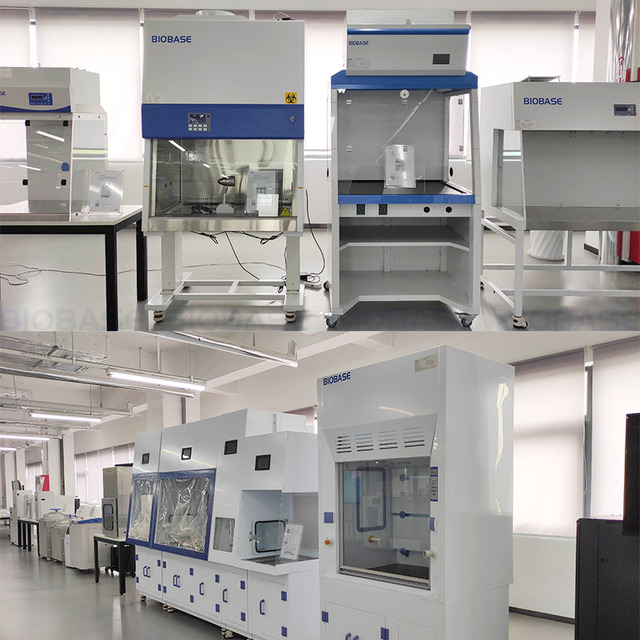
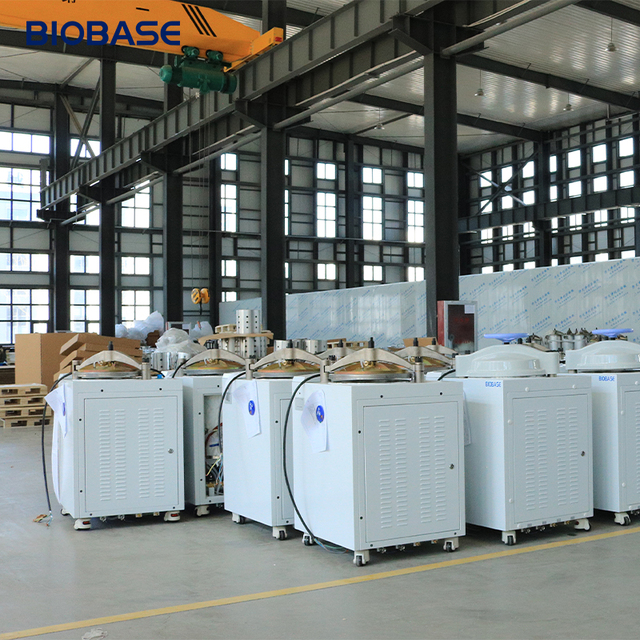
Overcoming geographical and supply chain barriers with integrated workflow design, local technical training, and tropicalization engineering.
From modular cleanroom isolation to microfluidic reader integration, we design customized laboratory layouts for hospital networks in Grenville. Our turnkey models minimize installation lead time and guarantee rapid operational readiness.
Navigating sea and air freight logistics into Grenville requires protective packaging. Our export packaging features hermetic moisture shielding, shock-absorbent framework, and temperature-monitored cold chain tracking for sensitive reagents.
We provide continuous medical education (CME) materials, virtual engineer onboarding, and rapid spare-part dispatch protocols to maintain 99.9% equipment uptime across all regional diagnostic stations in Grenville.
Anticipating future trends in point-of-care testing (mPOCT), AI-driven genetic analysis, and ultra-fast microfluidic chemistry.
Miniaturized thermal cyclers and microfluidic cartridges enable lab-quality nucleic acid amplification directly at point-of-care peripheral clinics in Grenville within 20 minutes, requiring minimal operational training.
Integrating automated deep-learning algorithms with karyotypic scanning software reduces optical identification times for chromosome anomalies, empowering pathology centers with unprecedented precision.
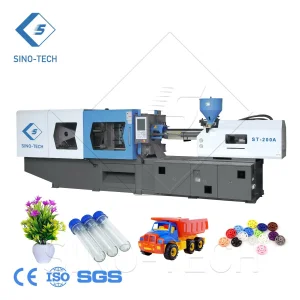
Deploying vacuum-sealed injection molded molecular tubes made from recyclable, bio-neutral polymers reduces biological plastic waste footprints while maintaining leak-proof integrity during transport.
Explore our complete range of certified diagnostic platforms, filling/capping packaging units, extractors, and assay kits available for Grenville importers.
Addressing standard operational inquiries regarding electrical compatibility, shipping, regulatory compliance, and system flexibility.
Yes. All systems shipped to Grenville are pre-configured with dual-voltage transformers (110V/220V, 50/60Hz) and heavy-duty internal surge suppression to guard against voltage fluctuations standard in island electrical grids.
Our manufacturing facilities operate under ISO 13485 (Medical Devices Quality Management Systems) and ISO 9001 certifications. Specific instruments and diagnostic kits maintain CE-IVD markings, ensuring compliance with rigorous European and global safety standards recognised by Grenville health authorities.
Yes, our real-time fluorescent PCR platforms and extraction equipment feature open-system channels. This allows laboratory technicians in Grenville to run standard commercial diagnostic kits as well as customized localized assays across standard optical channels (FAM, VIC/HEX, ROX, CY5).
Standard equipment lead time is 2 to 3 weeks following order confirmation. We provide complete export documentation including Certificates of Free Sale (CFS), Certificates of Origin (CO), Commercial Invoices, and Packing Lists to ensure expedited customs clearance at Grenville ports of entry.
Partner with a trusted global manufacturer. Connect with our engineering and procurement consultants to receive customized quotes, technical specifications, and laboratory workflow designs.
Send Inquiry Now Mosholu Medical